Tier-1 Product Specifications & Solutions
Explore our export-grade vinyl surfacing systems and industrial building panels. Rigorously tested for dimensional stability, water impermeability, and heavy traffic performance.
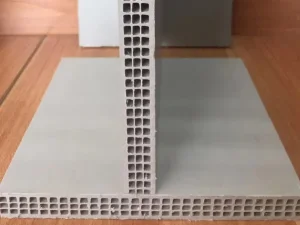
China PP Hollow plastic formwork panel 18mm for concrete Suppliers, Exporters
View Specifications
High-Quality Waterproof SPC Vinyl plastic flooring for indoor using Supplier, Exporter
View Specifications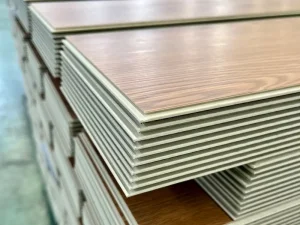
High-Quality Waterproof SPC flooring 4mm with marble and wood color Exporters, Service
View Specifications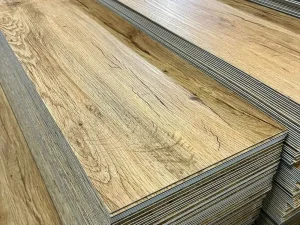
High-Quality Waterproof Plastic Vinyl LVT Glue Down Flooring Suppliers, Exporters
View Specifications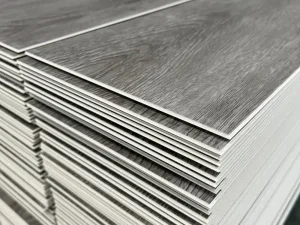
China SPC rigid vinyl plank with wood grain design for indoor flooring Supplier, Exporters
View Specifications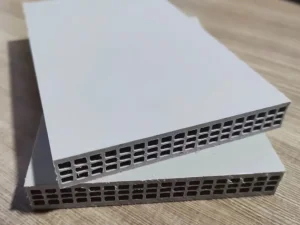
Wholesale PP Plastic Slab Concrete Hollow Formwork 18mm Exporters, Service
View Specifications
High-Quality Self-Adhesive Vinyl Tiles PVC LVT Plank Flooring Suppliers, Exporter
View Specifications
High-Quality LVT SPC Luxury Vinyl Tile Flooring for indoor using Exporter, Service
View SpecificationsGlobal Architectural Landscape & LVT Tile Effect Dynamics
An Analysis of Material Substitution Economics, Surface Tactility Evolution, and Commercial Specification Shifts in Modern Building Design.
The global architectural surfacing industry is experiencing a profound structural transition. For decades, natural stone, porcelain, and ceramic tiles held an unchallenged monopoly over high-traffic commercial and luxury residential flooring applications. However, structural constraints—including excessive dead-load weight on floor slabs, complex wet installation requirements, brittle impact mechanics, and elevated acoustic reflectance—have increasingly burdened commercial developers and general contractors.
In response, modern polymer engineering has elevated Luxury Vinyl Tile (LVT) tile effect flooring from a budget alternative to a primary, high-performance specification choice for architects, interior design firms, and global procurement directors. By mimicking the tactile depth, micro-vibrations, and aesthetic nuances of natural travertine, honed slate, polished concrete, and Italian marble, modern tile-effect LVT bridges the visual prestige of traditional masonry with the mechanical advantages of advanced polyvinyl chloride chemistry.
Acoustic & Impact Attenuation
Unlike rigid ceramic tiles that radiate impact sound (IIC ratings below 35 dB), high-density LVT tile effect planks integrated with acoustic underlays achieve IIC ratings exceeding 60–65 dB, drastically dampening footsteps in high-rise multi-family and hospitality environments.
Thermal Efficiency & Underfoot Ergonomics
Ceramic tiles create thermal sink effects, retaining cold and causing muscle fatigue during prolonged standing. Polymer-bound LVT tile effect flooring maintains room ambient temperatures and provides sub-millimeter elasticity, optimizing workplace ergonomics.
Rapid Installation Economics
Eliminating mortar mixing, expansion spacer setting, and 48-hour grout curing protocols, LVT click and glue-down systems reduce total project downtime by up to 65%, permitting immediate foot traffic after final rolling.
Key Industry Trend: The Shift Toward Embossed-in-Register (EIR) Micro-textures
The latest generation of LVT tile effect flooring utilizes digital sensor-aligned Embossing-in-Register (EIR) technology. By matching visual surface print nodes (grout lines, slate fissures, stone veins) with physical mechanical pressing rollers down to a 0.05mm tolerance, Chinese manufacturing hubs produce tile-effect surfaces virtually indistinguishable from quarried stone under dual-lighting spectrum inspection.
A rigorous examination of global B2B procurement queries reveals a clear evolution in user intent. Buyers are no longer searching merely for generic "cheap vinyl flooring." Search intent mining across North American, European, Middle Eastern, and Southeast Asian markets reveals highly specific, technical, and commercial criteria:
| Procurement Intent Category | Target Search Term Cluster | Primary Technical Benchmark Required | Decision-Maker Intent Level |
|---|---|---|---|
| Commercial Durability Verification | "0.7mm wear layer LVT stone effect", "Class 33 commercial vinyl tile" | Taber abrasion test > 50,000 cycles, UV-cured cross-linked polyurethane wear layer | High (General Contractors & Project Architects) |
| Environmental & Indoor Air Quality | "Low VOC LVT factory China", "Phthalate-free stone look vinyl" | FloorScore certification, CE EN 14041, REACH compliance, Zero-recycled filler purity | Critical (Institutional Buyers & Healthcare Specifiers) |
| Dimensional Stability under Heat | "SPC LVT click stone tile dimensional stability", "Anti-warping LVT tile" | Thermal shrinkage < 0.10% after 6 hours at 80°C (EN 434 / ISO 23999 standard) | High (Sunroom & Retail Developers) |
| OEM/ODM Supply Chain Agility | "China LVT flooring tile effect factory DIRECT", "Wholesale LVT container lead time" | Integrated R&D, 8+ automated production lines, 7-15 day dispatch, mixed-container loading | Immediate Purchase (Importers & Regional Brand Owners) |
Commercial buyers face localized economic pressures: tight construction windows, labor cost escalation in tile-setting trades (which can exceed $120/sq.m in Western markets), and strict municipal building energy conservation mandates. Consequently, procurement teams prioritize Chinese tier-1 suppliers who combine competitive FOB rates with complete technical compliance dossiers (ISO 9001, ISO 14041, CE, FloorScore, and ASTM testing reports).
China Industry 4.0: Supply Chain Resilience & Manufacturing Synergy
Inside Greenstar New Materials Shuyang Co., Ltd.: Automated Extrusion, Calendering Precision, and R&D Superiority.
At the center of China’s advanced vinyl flooring manufacturing landscape stands Greenstar New Materials Shuyang Co., Ltd. Located in Shuyang County, Suqian City, Jiangsu Province (First Floor, Office Building, No. 59 Dongfeng Road, Laozhuang Community, Sangxu Town), Greenstar has engineered a fully integrated manufacturing ecosystem that reconciles high throughput with ultra-precise chemical and mechanical quality controls.
Extrusion & Calendering Infrastructure
Greenstar operates 8 continuous high-capacity production lines capable of extruding high-density SPC rigid core boards and calendering multi-layer LVT vinyl sheets. By utilizing computer-controlled gravimetric dosing systems, raw virgin PVC polymer resin, natural limestone powder (CaCO3), and eco-friendly non-phthalate plasticizers are blended with exact stoichiometry, eliminating batch-to-batch density variations.
3,000㎡ R&D & Testing Laboratory
Spanning 3,000 square meters, Greenstar’s dedicated R&D testing center has formulated over 100 custom chemical variations. Every production batch undergoes rigorous quality assurance testing: thermal warping ovens, constant-temperature climate chambers (testing curl and shrinkage from -15°C to +80°C), micro-bevel shear strength tests, and color spectrophotometer spectrum mapping.
Furthermore, Greenstar’s strategic geographic location near major eastern Chinese maritime hubs (including Lianyungang, Qingdao, and Shanghai ports) enables streamlined logistical routing. Typical order processing to vessel loading is compressed to 7–15 days, guaranteeing unparalleled supply chain agility for international distributors facing tight construction milestones.
To maximize information value for project engineers and procurement personnel, the following matrix outlines specialized installation scenarios for LVT tile-effect systems alongside recommended technical parameters:
1. Luxury Hospitality Lounges & Boutique Hotel Lobbies
Target Aesthetic: Honed White Carrara Marble or Soft Travertine Tile Effect.
Recommended Spec: 2.5mm – 3.0mm Dry Back Glue-Down LVT, 0.5mm Wear Layer, Ceramic Bead UV Coating, Painted Micro-Bevel edges.
Engineering Rationale: Glue-down installation eliminates hollow acoustic reverberation under luggage wheels and high heels while permitting isolated tile replacement in heavy-wear zones.
2. Healthcare Clinics, Aseptic Labs & Cleanrooms
Target Aesthetic: Seamless Light Grey Monolithic Concrete or Terrazzo Effect.
Recommended Spec: 3.0mm Loose Lay or Glue-Down LVT, 0.7mm Heavy Commercial Wear Layer, Silver-Ion Anti-Bacterial Surface Coating.
Engineering Rationale: Chemical resistance to iodine, alcohol disinfectants, and hospital cart castor loads. Non-porous surface structure prevents microbial colonization in seams.
3. High-Traffic Retail Malls & Supermarkets
Target Aesthetic: Dark Industrial Slate or Charcoal Basalt Tile Effect.
Recommended Spec: 5.0mm – 6.0mm SPC Rigid Core Click Tile (or 3.0mm Glue-Down), 0.7mm Wear Layer, Anti-Slip Rating R10/DS class.
Engineering Rationale: Extreme resistance to static point loading (display racks) and dynamic rolling loads (cleaning machines and shopping carts) without indentation failures.
4. Multi-Family Residential Build-to-Rent (BTR)
Target Aesthetic: Warm Beige Calacatta or Modern Greige Limestone Effect.
Recommended Spec: 4.0mm SPC Click Tile with 1.0mm pre-attached IXPE sound insulation pad.
Engineering Rationale: Rapid click-lock floating installation directly over imperfect subfloors; 100% waterproof protection against tenant spills, pet accidents, and bathroom humidity.
Technical Buyer's Specification & Quality Evaluation Guide
Avoid Costly Procurement Errors: Factory Testing Parameters Every Importer Must Audit.
When sourcing LVT tile-effect products from China, procurement engineers must evaluate technical test certificates rather than relying solely on visual samples. Below is the technical audit protocol utilized by Greenstar's quality assurance division:
1. Wear Layer Thickness Verification
Verify wear layer caliber using optical micrometers. Residential specifications require 0.2mm–0.3mm; general commercial requires 0.5mm; heavy industrial/healthcare mandates 0.7mm. Ensure a double UV coating layer containing microscopic ceramic beads (Al2O3) is applied for scratch mitigation.
2. Dimensional Stability & Thermal Memory
Subject samples to ISO 23999 thermal cycling (80°C for 6 hours). Premium virgin-resin LVT exhibits dimensional variation under 0.08% and residual curling under 0.15mm. High levels of recycled plastic fillers increase thermal expansion rates, resulting in joint tenting in summer and seam gapping in winter.
3. Phthalate & Chemical Emissions Audit
Ensure compliance with REACH Regulation (EC) No 1907/2006. Low-grade plasticizers (such as DEHP, DBP, BBP) off-gas harmful VOCs. Greenstar utilizes certified non-phthalate DOTP plasticizers, achieving FloorScore and AgBB certifications for ultra-low indoor air emissions.
Frequently Asked Questions (B2B Procurement Q&A)
Direct Answers from Our Engineering & Technical Sales Teams for Global Importers and Contractors.
What is the exact distinction between LVT Tile Effect flooring and SPC Stone Effect flooring?
LVT (Luxury Vinyl Tile) relies on a flexible, multi-layered virgin PVC structure with printed decor films and wear layers, making it softer, quieter underfoot, and typically installed via glue-down or loose-lay adhesive methods. SPC (Stone Plastic Composite) features a rigid core composed of approximately 60-70% calcium carbonate (limestone powder) combined with PVC resin. SPC offers extreme core rigidity, 100% waterproof stability, high resistance to subfloor telegraphing, and utilizes click-lock floating installation system profiles.
How does LVT tile-effect flooring compare to real ceramic or porcelain tiles in installation cost?
While material costs vary by grade, the overall installed cost of tile-effect LVT is typically 40% to 60% lower than natural stone or ceramic tiles. Ceramic installations require expensive surface grinding, wet mortar, specialized tile setters, expansion joint placement, and long curing times. LVT tile effect planks can be laid over existing flat substrates rapidly using pressure-sensitive adhesives or click systems, dramatically lowering site labor expenses and downtime.
What design customization options (OEM/ODM) are available at Greenstar's facility?
Greenstar offers end-to-end OEM and ODM customization. Importers can select custom decorative film prints (including slate, concrete, terrazzo, marble, and travertine), specify custom tile dimensions (e.g., 12"x24", 18"x36", 24"x24", or hexagonal cuts), adjust wear layer thickness (0.2mm to 0.7mm), incorporate custom UV surface lamination (ultra-matte, gloss, or anti-bacterial), and order private-label packaging boxes with custom branding and barcode printing.
What is Greenstar's standard production capacity and dispatch lead time for export containers?
With 8 automated production lines operating continuously, Greenstar maintains a monthly output capacity exceeding 300 FCL containers. Standard catalog specifications can be manufactured, packed, and dispatched to nearby port facilities within 7 to 15 days following order confirmation and deposit settlement.
How do you verify panel quality and performance for plastic shuttering formwork products?
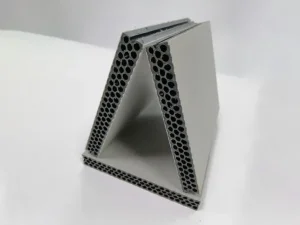
For PP hollow plastic formwork panels used in concrete construction, quality is assessed by sheet weight consistency (verifying density), surface rib wall thickness, impact resistance at low temperatures, and reuse cycle capability. High-grade PP formwork panels withstand more than 50-60 reuses without swelling, delamination, or warping under severe summer heat and winter cold conditions.
Are samples available prior to issuing a commercial purchase order?
Yes. Express sample kits are dispatched globally via courier service (DHL/FedEx/UPS). Sample boxes include physical color chips, wear layer cross-section cutaways, click-lock joinery demonstrations, and official lab testing documentation so procurement officers can audit material quality before committing to bulk container orders.
What international environmental certifications do Greenstar products comply with?
All Greenstar flooring product ranges comply with international safety and environmental directives, including CE EN 14041 certification, FloorScore Indoor Air Quality testing, REACH non-toxic compliance, and ISO 9001 / ISO 14001 factory management standards, ensuring smooth customs clearance across European, North American, and Australasian customs jurisdictions.
Featured Industrial Collections & Order Specifications
Browse our complete export catalog items below. Click any button to view full technical datasheets and initiate wholesale container inquiries.
High-Quality Waterproof SPC Vinyl plastic flooring for indoor using Supplier, Exporter
View Specifications
High-Quality Waterproof SPC flooring 4mm with marble and wood color Exporters, Service
View Specifications
High-Quality Waterproof Plastic Vinyl LVT Glue Down Flooring Suppliers, Exporters
View Specifications
China SPC rigid vinyl plank with wood grain design for indoor flooring Supplier, Exporters
View Specifications
Wholesale PP Plastic Slab Concrete Hollow Formwork 18mm Exporters, Service
View Specifications
High-Quality Self-Adhesive Vinyl Tiles PVC LVT Plank Flooring Suppliers, Exporter
View Specifications
High-Quality LVT SPC Luxury Vinyl Tile Flooring for indoor using Exporter, Service
View Specifications