High-Performance LVT & SPC Flooring Catalog
Direct factory supply featuring advanced wear layers, stone/wood optics, and engineered core stability.
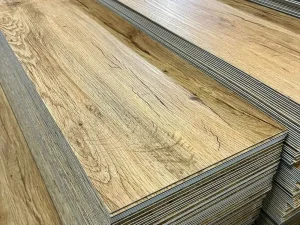
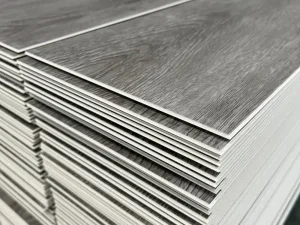
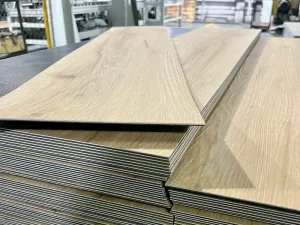
The Macro Paradigm Shift: LVT Tile Effect Flooring in Modern Architecture
Why international commercial developers and institutional buyers are systematically transitioning from traditional ceramic, porcelain, and natural slate to engineered Luxury Vinyl Tile (LVT) with stone and ceramic aesthetics.
Thermal Efficiency & Subfloor Damping
Unlike natural marble or porcelain tiles, which exhibit high thermal conductivity and cold underfoot feel, LVT tile effect planks integrate viscoelastic polymer layers. This provides superior thermal insulation (R-value optimization) and dampens impact noise (delta IIC acoustic performance) in multi-story commercial buildings.
Structural Load Reduction
Traditional 10mm ceramic tiles weigh roughly 20–25 kg/m², posing significant dead-load constraints for high-rise developments. LVT stone-effect tiles deliver identical visual aesthetics at just 4–7 kg/m², reducing structural stress, simplifying freight handling, and decreasing container shipping tonnage.
Zero-Grout Sanitary Assurance
Tile grout lines are inherently porous, harboring bacteria, moisture, and mildew in high-footfall or wet environments. Precision-engineered LVT tile effect flooring utilizes click-lock or tight butt-joint glue-down systems, creating a seamless, hygienic surface compliant with stringent healthcare and hospitality sanitation guidelines.
Anatomy of Next-Gen LVT Tile Effect Flooring
Understanding the multi-layer cross-linked polymer architecture engineered inside China's leading export-grade vinyl factories.
1. PUR Ceramic-Bead Coating
A double-cured Polyurethane (PUR) surface treatment embedded with microscopic ceramic beads (silicon carbide / aluminum oxide). Provides ultra-high scratch resistance, anti-stain defense against petroleum/chemicals, and UV-stabilization to eliminate color fading under intense direct sunlight.
2. Embossed Micro-Bevel Wear Layer
Ranging from 0.3mm (residential) to 0.55mm / 0.70mm (heavy commercial/industrial), this virgin PVC wear layer undergoes Embossed-in-Register (EIR) pressing. It mirrors the exact tactile clefts, matte quartz stone grain, and travertine fissures of natural stone.
3. HD Photorealistic Slate/Marble Film
High-definition rotogravure printing technology capturing true 3D visual depth of Carrara marble, concrete screed, terrazzo, and dark slate. Advanced color mixing ensures up to 30 unique tile patterns per batch, preventing repetitive visual cues over large commercial expanses.
4. Fiber-Reinforced Calendered Core
The core layer utilizes high-density virgin PVC combined with non-phthalate plasticizers and an embedded non-woven fiberglass mesh layer. This eliminates thermal expansion or contraction, ensuring dimensional stability across extreme temperature fluctuations (-10°C to +60°C).
5. Precision Locking Mechanism
Machined using German HOMAG double-end tenoner systems, the click-lock profiles (Uniclic, Valinge 2G/5H) ensure tight tolerance matching within 0.02mm. This structural rigidity prevents vertical disengagement under heavy rolling loads such as hospital beds and shopping carts.
6. Integrated Acoustic Underlayment
Factory-laminated IXPE (Irradiated Cross-linked Polyethylene) or high-density EVA foam backing (1.0mm - 2.0mm). Provides instant sound insulation up to 21dB, conceals minor subfloor imperfections, and reduces installer labor costs on site.
China's Factory Efficiency & Export Advantage
How Chinese LVT flooring manufacturers leverage integrated industrial supply chains, advanced automation, and strict quality control to deliver global cost-performance leadership.
Integrated Chemical & Polymer Clusters
China’s specialized manufacturing hubs in Jiangsu, Zhejiang, and Shandong bring PVC resin synthesizers, eco-friendly plasticizer producers, photo-film printers, and diamond-tooling suppliers within a 50km radius. This hyper-localized supply chain dramatically reduces raw material transit costs, mitigates global logistics friction, and enables fast factory-to-port turnaround within 7 to 15 business days.
- Direct bulk sourcing of high-purity virgin PVC resin
- Custom formulation of heavy-metal-free, low-VOC stabilizers
- Instant production scale-up supporting multi-container orders
Automated Hot-Pressing & AI Optical QC
Leading Chinese exporters deploy automated multi-daylight hydraulic hot-press systems operating under computerized temperature and pressure profiling. Integrated AI machine-vision inspection scanners monitor decor alignment, edge straightness, surface micro-defects, and color consistency in real time across 100% of production runs, ensuring zero batch-to-batch deviation.
- Zero-defect optical laser scanning along profile edges
- Precise core density control (1900–2100 kg/m³ for SPC/LVT hybrids)
- Automated robot palletizing & moisture-proof shrink packaging
Targeted Sector Deployments & Performance Scenarios
LVT tile effect flooring is engineered to solve specific physical challenges across high-demand commercial, institutional, and residential environments.
High-Traffic Retail
Heavy footfall, rolling display racks, and frequent spillages demand a minimum 0.55mm wear layer. Slate and terrazzo LVT tiles create a high-end boutique ambience without the risk of cracked ceramic tiles from dropped merchandise.
Luxury Hospitality
Hotel lobbies and dining spaces require rapid overnight renovation capability. Loose-lay or click-lock marble-effect LVT can be installed directly over existing floor structures with zero downtime and acoustic quietness.
Healthcare & Cleanrooms
Seamless installation prevents moisture entrapment beneath beds. Chemical-resistant PUR coatings withstand aggressive hospital-grade disinfectants and stain agents (iodine, alcohol, blood) without surface erosion.
Multi-Family Residential
Concrete-look LVT tiles give modern apartment developments an urban industrial aesthetic. The integrated IXPE underlay meets strict inter-floor acoustic sound transmission standards (STC & IIC ratings).
Development Trends & Next-Gen Innovations
How emerging technological paradigms are shaping the next decade of resilient synthetic stone flooring manufacturing.
Direct-to-Core Digital Printing
Eliminating decorative film layers by applying ultra-high resolution digital inkjet printing directly onto the primed vinyl/SPC core. Allows infinite visual variation, custom branding, and zero pattern repeat across unlimited floor areas.
Bio-Based Plasticizers & Circularity
Transitioning from petroleum-derived plasticizers to soybean and castor oil bio-based alternatives. Chinese factories are implementing closed-loop post-industrial recycling programs, reintegrating clean factory offcuts into core layers.
Ultra-Matte Low-Gloss Finishes
Global architectural demand has shifted away from high-gloss simulated stone toward ultra-matte (3–5% gloss level) micro-textured surfaces. Advanced electron-beam (EB) curing yields ultra-durable matte textures that resist fingermarks and smudge stains.
Global Procurement & Risk Mitigation Framework
A strategic checklist for overseas importers, wholesalers, and general contractors sourcing LVT tile effect flooring from Chinese exporters.
1. Critical Testing & International Certifications
Before issuing a Purchase Order (PO), verify that the manufacturer holds independent third-party laboratory test reports (SGS, Intertek, TÜV Rheinland) covering the following mandatory standards:
- ISO 10582 / ASTM F1700: Specification for resilient vinyl tile standards.
- EN 13501-1 / ASTM E648: Fire reaction testing (Bfl-s1 critical radiant flux rating).
- FloorScore / DIBt / AgBB: Low volatile organic compound (VOC) indoor air quality compliance.
- DIN 51130 / BS 7976-2: Slip resistance pendulum testing (R9 - R11 ratings).
2. Container Loading & Freight Optimization
Because resilient flooring is heavy and dense, freight cost optimization relies on maximizing container weight limits without exceeding port axle regulations:
- 20FT Heavy Container Strategy: Load up to 21–27 metric tons depending on destination port allowance.
- Palletization Guarding: Fumigated plywood pallets with plastic edge protectors and heavy-duty steel strapping.
- Moisture Control: In-container desiccant packs to eliminate ocean condensation ("container rain") during transit.
Frequently Asked Questions
Expert answers to common technical, commercial, and logistical inquiries regarding LVT tile effect flooring sourcing.
What is the technical difference between Glue-Down LVT Tile Effect and Click-Lock SPC Tile Flooring?
Glue-Down LVT consists of flexible, 100% vinyl layers (typically 2.0mm–3.0mm thick) that require full-spread adhesive application over a perfectly smooth subfloor. It is highly cost-effective for large commercial projects and easy to replace plank-by-plank. Click-Lock SPC (Stone Plastic Composite) features a rigid core made of limestone powder and PVC stabilizer (typically 4.0mm–6.5mm thick). It offers superior dimensional stability, conceals minor subfloor imperfections, incorporates click installation without glue, and provides 100% waterproof performance in high-moisture environments.
How does LVT tile effect flooring perform under heavy commercial rolling loads?
High-grade commercial LVT tile flooring with a wear layer of 0.55mm (22mil) or 0.70mm (28mil) and a high-density virgin core is engineered to withstand heavy static and rolling loads according to ASTM F970 standards (withstanding static load pressures exceeding 250 psi to 1500 psi). For environments with heavy rolling hospital beds or forklift traffic, a direct glue-down installation using hard-set acrylic adhesive is recommended to eliminate plank displacement.
Can LVT stone-effect tiles be installed over existing ceramic tiles?
Yes. Rigid core click-lock LVT and SPC tile flooring can be installed directly over existing ceramic or porcelain tiles provided the existing floor is structurally sound and flat (within 3mm per 2 meters). If grout lines are wider than 5mm or deeper than 3mm, they should be skim-coated with a cementitious self-leveling patch compound to prevent joint telegraphing over time.
What minimum order quantity (MOQ) and lead times do Chinese exporters typically require?
Standard factory MOQs for custom color matches or specific wear-layer configurations usually range from 500 m² to 1,000 m² per color decor. For standard stocked decor collections, MOQs can be as low as 200 m² or combined across mixed-decor full container loads (FCL). Average factory production lead times range from 7 to 15 days upon deposit confirmation and sample approval.
Is LVT tile effect flooring suitable for subfloor underfloor heating (UFH) systems?
Yes, virgin PVC LVT tile flooring is fully compatible with both hydronic (water) and electric radiant underfloor heating systems. The maximum recommended subfloor surface operating temperature is 27°C (80°F). The low thermal resistance (R-value) of LVT ensures rapid heat transfer, making it more energy-efficient than wood or thick carpet overlayment.
How does EIR (Embossed-in-Register) technology enhance tile-look LVT visual authenticity?
EIR utilizes state-of-the-art optical sensors to synchronize the physical mechanical embossing rollers directly with the visual print pattern of the decorative film layer. When the image displays a marble vein, travertine pore, or concrete fissure, the physical surface texture matches that precise coordinate, creating a realistic tactical experience virtually indistinguishable from real stone.
What warranties are supplied by China direct exporters for commercial projects?
Professional Chinese manufacturers provide structured factory warranties backed by laboratory performance testing. Residential applications typically carry a 15-year to 25-year wear warranty, while heavy commercial installations with a 0.55mm wear layer carry a 10-year to 15-year limited commercial wear and structural integrity warranty.
Explore Complete Flooring & Construction Solutions
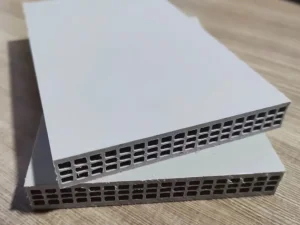
Direct factory supply featuring SPC, LVT, and engineered construction panels for global infrastructure and interior projects.
Partner with China's Premier LVT & Flooring Exporters
Get direct access to OEM/ODM custom specifications, physical swatch kits, technical data sheets, and real-time container FOB pricing direct from our factory engineers.
Connect with Engineering Export Team