Featured SPC & LVT Commercial Flooring Solutions
Explore our top-export engineered vinyl flooring systems and heavy-duty building components crafted to rigorous international structural and environmental standards.
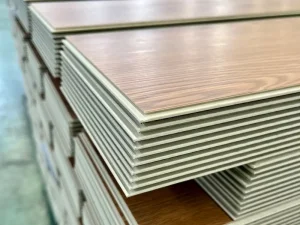
High-Quality Waterproof SPC flooring 4mm with marble and wood color Exporters, Service
View Details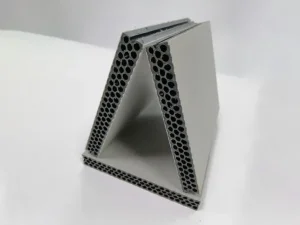
Wholesale Reusable plastic concrete shuttering formwork for construction building Supplier, Exporters
View Details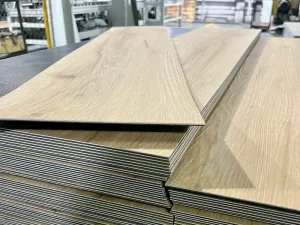
High-Quality LVT SPC Luxury Vinyl Tile Flooring for indoor using Exporter, Service
View Details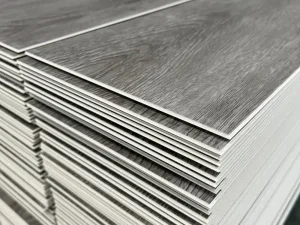
China SPC rigid vinyl plank with wood grain design for indoor flooring Supplier, Exporters
View Details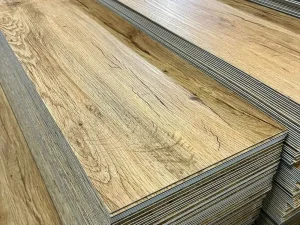
High-Quality Waterproof Plastic Vinyl LVT Glue Down Flooring Suppliers, Exporters
View Details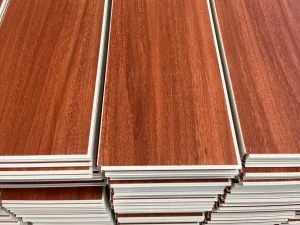
High-Quality Waterproof SPC Vinyl plastic flooring for indoor using Supplier, Exporter
View Details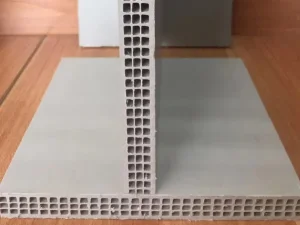
China PP Hollow plastic formwork panel 18mm for concrete Suppliers, Exporters
View Details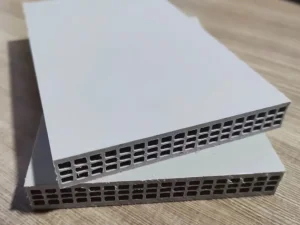
Wholesale PP Plastic Slab Concrete Hollow Formwork 18mm Exporters, Service
View Details1. Executive Overview: The Engineering Evolution of SPC and LVT Flooring
Over the past decade, the global architectural surfaces market has experienced a seismic shift from traditional hardwood, laminate, and ceramic tiles toward high-performance resilient flooring—specifically Stone Plastic Composite (SPC) and Luxury Vinyl Tile (LVT).
Material Science Innovation
SPC flooring utilizes an ultra-dense rigid core engineered from a precise ratio of natural limestone powder (calcium carbonate, CaCO3), polyvinyl chloride (PVC) resin, and eco-friendly non-phthalate stabilizers. This dense composite structure eliminates plasticizer telegraphing and ensures complete dimensional stability across wide temperature variations (-20°C to 70°C).
Precision Click Locking Geometry
Modern SPC click flooring integrates licensed patented profiling systems such as Unilin and Välinge (2G/5G/5Gi). Precision-milled joints facilitate seamless glueless installation, vastly reducing labor overhead, speeding up project turnaround, and achieving vertical locking tension strength exceeds 2.0 kN/m.
Total Lifecycle Economics
While traditional timber or stone require costly maintenance, sealants, and moisture protection, SPC and LVT systems provide 100% waterproof protection, high flame retardancy (Class Bfl-s1), extreme scratch resistance (up to 0.7mm wear layer + UV ceramic bead coating), and low lifecycle cost for large commercial facilities.
2. Architectural Specifications & Resilient Product Comparison
To assist global procurement directors, structural engineers, and flooring distributors in selecting the appropriate substrate technology, the comparative matrix below outlines structural parameters across resilient flooring categories.
| Performance Criteria | SPC Click Rigid Core | LVT Dry Back (Glue Down) | LVT Click (Flexible) | WPC Flooring |
|---|---|---|---|---|
| Primary Composition | 70% Limestone (CaCO3) + 30% Virgin PVC Resin | Polyvinyl Chloride Resin + Plasticizers + Fillers | Multi-layer PVC Vinyl with Fiberglass Core | PVC Resin + Wood Flour + Foaming Agents |
| Typical Thickness Range | 3.5mm – 7.0mm (Excl. Underlayment) | 2.0mm – 3.0mm | 4.0mm – 5.0mm | 5.5mm – 8.0mm |
| Wear Layer Thickness Options | 0.3mm (12mil) to 0.7mm (28mil) Ceramic Bead Coating | 0.12mm (5mil) to 0.5mm (20mil) | 0.3mm (12mil) to 0.5mm (20mil) | 0.3mm (12mil) to 0.7mm (28mil) |
| Dimensional Stability (ISO 23999) | Superior (≤0.08%) – No Curling under Direct Sunlight | Moderate (≤0.15%) – Requires Strict Adhesives | Moderate (≤0.15%) – Subject to Thermal Expansion | Good (≤0.10%) – Temperature Sensitive |
| Subfloor Imperfection Tolerance | High – Bridges Subfloor Irregularities (≤2mm/2m) | Low – Subfloor Telegraphing Will Occur Without Levelling | Moderate – Requires Flat Subfloor Surface | High – Soft Foamed Core Masks Minor Defects |
| Impact Sound Insulation (IIC / STC) | IIC 68 – 72 dB (With 1.5mm Attached IXPE Foam) | IIC 45 – 50 dB (Direct Subfloor Contact) | IIC 55 – 60 dB (Dependent on Underlay) | IIC 62 – 65 dB (Cellular Foamed Core) |
| Installation Method & Speed | Floating Click (Unilin/Välinge) – 120 sqm/day/person | Full-spread Adhesive – Labor Intensive (50 sqm/day) | Floating Click – Moderate Speed (80 sqm/day) | Floating Click – Fast Installation |
| Environmental Certifications | FloorScore, GREENGUARD Gold, CE Marking, REACH | FloorScore, CE Marking | FloorScore, CE Marking | FloorScore, GREENGUARD Gold |
3. China's Direct Factory Supply Chain & Manufacturing Ecosystem
China remains the world's undisputed center for resilient flooring production, driven by integrated upstream raw material clusters, advanced multi-extrusion equipment, and rigorous quality verification protocols.
Shuyang, Jiangsu Supply Hub
Situated in Shuyang, Suqian City—one of Eastern China’s premier industrial material bases—manufacturing facilities benefit from localized access to ultra-pure limestone deposits, PVC monomer plants, high-definition decorative print film mills, and world-class shipping hubs near Shanghai and Lianyungang ports.
Automated Multi-Extrusion Lines
Equipped with 8+ modern high-speed twin-screw co-extrusion lines, automated annealing ovens, infrared-controlled tempering channels, and dynamic multi-blade slitting machinery, our production throughput yields over 100,000 square meters per day with millimetric precision thickness tolerance (±0.05mm).
End-to-End Quality Assurance
Every production batch undergoes strict QA testing: 24-hour water immersion swell testing, boiling water dimensional stability tests (80°C for 6 hours), mechanical wear layer abrasion cycles (Taber Abraser test), and zero-defect click profile tension testing using optical shadowgraphs.
4. Strategic Sourcing Criteria for Global Commercial Buyers
For international importers, real estate developers, and big-box distributors, procuring SPC and LVT flooring directly from China requires evaluating key technical criteria to ensure project compliance and minimize import risks.
1. Embossed-in-Register (EIR) Surface Technology
Commercial buyers increasingly require 3D EIR texture mapping where the surface micro-embossing precisely matches the underlying natural wood grain or stone print film pattern. This eliminates artificial plastic luster, yielding realistic timber aesthetics without compromising heavy commercial wear ratings.
2. Underlay Acoustic Integration (IXPE vs EVA)
Factory-attached sound reduction underlays (1.0mm, 1.5mm, or 2.0mm high-density IXPE foam) reduce field labor costs by up to 40%. Closed-cell IXPE offers superior mold resistance, zero moisture absorption, and excellent Impact Insulation Class (IIC) acoustic dampening compared to standard EVA options.
3. Container Density & Export Packaging Optimization
Due to the high density of SPC rigid cores (~2.0 g/cm³), freight efficiency depends on optimal weight-to-volume container planning. High-strength shrink-wrapped corrugated cartons, solid fumigated wooden pallets, and moisture-proof plastic wrapping guarantee zero edge damage during transoceanic shipping.
4. Tariff Classification & Compliance Guidance
Navigating HS codes (e.g., HS 3918.10 for vinyl floor coverings) and country-of-origin documentation (Form E, Certificate of Origin, anti-dumping documentation) is critical. OEM/ODM exporters provide tailored packing lists, commercial invoices, and tariff strategy guidance to ensure smooth port customs clearances.
5. Regional Application Scenarios & Compliance Standards
Flooring performance needs vary significantly across climatic zones, building codes, and regional installation habits. Our production formulations are optimized for localized application environments worldwide.
North America (US & Canada)
Focus: Heavy wear resistance, FloorScore indoor air quality certification, compliance with ASTM F2199 (dimensional stability) and ASTM E648 (critical radiant flux). Ideal for multi-family residential housing, hospitality franchises, and retail chains demanding strict phthalate-free safety.
European Union & UK
Focus: CE Marking (EN 14041), French VOC Regulation (Class A+), AgBB emissions standards, and REACH SVHC compliance. Demands tight click profile tolerances for DIY and professional floating installations across severe seasonal temperature swings.
Middle East, SE Asia & Tropics
Focus: High-heat resistance (>70°C oven testing), UV anti-fading ceramic topcoats, and 100% moisture immunity. Designed to resist warp, cupping, or lock disengagement in high-humidity coastal and arid hot environments.
6. Future Trends in SPC & Resilient Surface Innovations
Continuous R&D is shaping the next generation of vinyl and composite surfaces. Discover the key technological advancements driving modern building projects.
Ultra-Matte Anti-Scratch Nano Surfaces
Traditional glossy polyurethane finishes are giving way to advanced electron-beam cured nano ceramic finishes with matte shine levels (<5 G.U.). These coatings deliver exceptional micro-scratch resistance, eliminate glare, and resist stubborn scuffs from footwear and heavy furniture.
Acoustic Bio-Core Innovations
Integration of lightweight mineral-organic matrix cores and recycled bio-polymers reduces overall board weight by up to 15% without compromising impact strength or lock integrity, lowering container transit carbon footprints globally.
Formwork & Substrate Resource Synergy
In large-scale commercial real estate development, cross-material supply chain integration—such as pairing high-performance SPC interior flooring with reusable PP hollow plastic concrete formwork panels (18mm)—streamlines project procurement, reduces waste, and lowers building material costs.
7. Frequently Asked Questions (FAQ) for Global Buyers
Detailed answers to technical, logistics, and quality assurance queries commonly raised by international importers, distributors, and procurement engineers.
What is the structural difference between SPC flooring and traditional LVT?
SPC (Stone Plastic Composite) flooring features a solid, rigid core made of approximately 70% natural limestone powder (CaCO3) combined with PVC resin and thermal stabilizers. This renders the plank extremely rigid, highly impact-resistant, and 100% dimensionally stable under heat. Traditional LVT (Luxury Vinyl Tile) utilizes a flexible multi-layer PVC structure. While flexible LVT is comfortable underfoot and excellent for glued-down commercial applications, SPC rigid core can be floated over imperfect subfloors without telegraphing minor substrate flaws.
How do you guarantee click lock profile strength and avoid disengagement?
We utilize precision CNC diamond cutters licensed by Unilin and Välinge to profile our click locking systems (2G, 5G, 5Gi). Our strict milling tolerances (±0.02mm) undergo continuous laser shadowgraph inspection during production. Furthermore, our formulation optimizes core elasticity to prevent brittle tongue fractures while maintaining vertical tensile lock strength well above 2.0 kN/m.
What certifications are provided for environmental and indoor air quality compliance?
Our complete resilient flooring portfolio complies with strict international environmental standards. Products are certified FloorScore, GREENGUARD Gold, CE Marked (EN 14041), and verified 100% phthalate-free under EU REACH regulations. Test reports for formaldehyde emission (E1/E0 class), heavy metals, and critical radiant flux fire safety (Class Bfl-s1) are provided per container batch.
Can SPC flooring be installed over underfloor heating systems?
Yes. Due to its high inorganic mineral content (limestone) and superior dimensional stability (≤0.08% expansion rate under ISO 23999 testing), SPC flooring is ideal for embedded hydronic or electric underfloor heating systems. We recommend maintaining a maximum subfloor surface temperature of 27°C (80°F) and utilizing high-density closed-cell IXPE underlayment for optimal heat transfer.
What is the minimum wear layer thickness recommended for heavy commercial installations?
For high-traffic commercial environments such as hotel lobbies, hospital corridors, retail centers, and office complexes, a minimum wear layer of 0.5mm (20mil) or 0.7mm (28mil) with double UV ceramic bead coating is recommended. For residential and light commercial multi-family apartments, a 0.3mm (12mil) wear layer provides excellent durability with long warranty protection.
What are the lead times and minimum order quantities (MOQ) for custom OEM orders?
Standard lead time for FCL (Full Container Load) production is typically 7 to 15 days from deposit confirmation, backed by our 8 continuous extrusion lines. Our standard MOQ is 500 square meters per decor color for stocked film patterns, and 1,000 square meters for fully customized private label packaging and bespoke color development.
Explore Our Full Range of Exported Materials
All original product items are fully preserved below. Click any button to view detailed product specifications and request custom manufacturing quotes.
High-Quality Waterproof SPC flooring 4mm with marble and wood color Exporters, Service
View Product
Wholesale Reusable plastic concrete shuttering formwork for construction building Supplier, Exporters
View Product
High-Quality LVT SPC Luxury Vinyl Tile Flooring for indoor using Exporter, Service
View Product
China SPC rigid vinyl plank with wood grain design for indoor flooring Supplier, Exporters
View Product
High-Quality Waterproof Plastic Vinyl LVT Glue Down Flooring Suppliers, Exporters
View Product
High-Quality Waterproof SPC Vinyl plastic flooring for indoor using Supplier, Exporter
View Product
China PP Hollow plastic formwork panel 18mm for concrete Suppliers, Exporters
View Product
Wholesale PP Plastic Slab Concrete Hollow Formwork 18mm Exporters, Service
View Product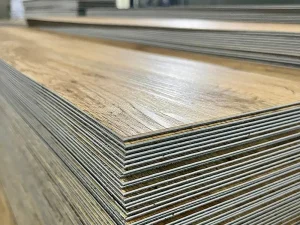
High-Quality Self-Adhesive Vinyl Tiles PVC LVT Plank Flooring Suppliers, Exporter
View ProductPartner with China's Premier SPC & LVT Manufacturer
Request factory-direct samples, technical documentation, or customized FCL container pricing tailored to your market specifications.
Contact Technical Sales Team