Factory-Direct Wood-Look Vinyl & Structural Solutions
Explore our core engineering items exported to over 40 countries for commercial real estate, multi-family developments, and heavy construction.
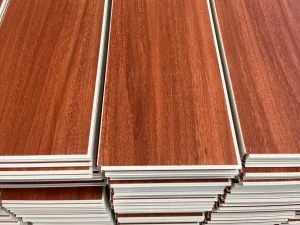
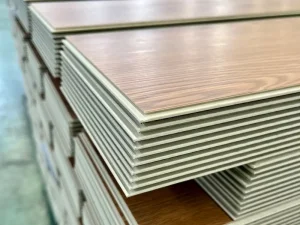
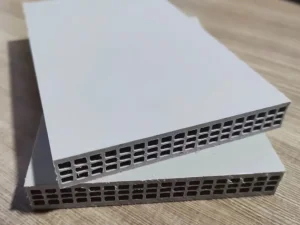
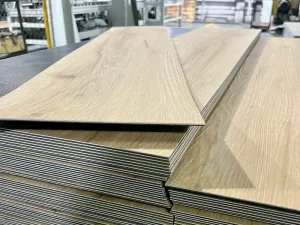
1. Executive Summary: The Technical Evolution of Wood-Look Vinyl Flooring
In modern architectural design and commercial facility procurement, wood-look flooring continues to lead globally due to its universal aesthetic appeal. However, natural hardwood flooring presents significant operational vulnerabilities: moisture absorption leading to volumetric expansion, susceptibility to termite infestation, high lifecycle maintenance costs, and strict acoustic limitations in multi-family and hospitality structures. Over the past decade, engineered resilient flooring—specifically Luxury Vinyl Tile (LVT) and Stone Plastic Composite (SPC) rigid core flooring—has disrupted the commercial flooring landscape, capturing over 40% of global commercial surface specification share.
As a leading wholesale vinyl tile that looks like wood supplier and exporter, our enterprise integrates advanced polymer formulation, ultra-high-definition Embossed-in-Register (EIR) optical texturing, and precision German click-lock milling technology. This whitepaper serves as an exhaustive technical guide for procurement managers, architects, importers, and general contractors seeking high-information gain regarding material physics, manufacturing paradigms, supply chain economics, and global specification standards.
100% Hydrophobic Core
Unaffected by standing water or elevated subfloor moisture emissions (up to 95% RH under ASTM F2170), eliminating mold proliferation and plank cupping.
Micro-Scratch Ceramics
Proprietary double UV polyurethane coating infused with microscopic aluminum oxide beads, delivering commercial wear resistance up to 28 mil (0.7mm).
Rapid Click System
Engineered Unilin and Välinge 5G drop-lock click profiles milled to a tolerance of ±0.02mm, cutting on-site installation labor costs by up to 60%.
2. Why China's Manufacturing Infrastructure Leads Global Vinyl Tile Supply
The global sourcing hub for resilient vinyl flooring is concentrated within Chinese manufacturing clusters, specifically across Jiangsu and Zhejiang provinces. The structural competitive advantage of Chinese factories extends beyond low labor costs; it stems from an unmatched supply chain ecosystem that integrates raw material refining, extrusion machinery fabrication, decorative film printing, click-profile precision tooling, and international port logistics within a 100-kilometer radius.
Core Industrial Cluster Advantages:
1. Vertical Material Integration: China produces high-purity virgin PVC resin and fine-milled limestone powder locally. This immediate proximity guarantees consistent batch-to-batch chemical stability, preventing core discoloration and density variances common in decentralized global supply chains.
2. Advanced Co-Extrusion Technology: Leading factories in China utilize high-torque twin-screw extruders operating with automated gravimetric dosing systems. This allows for continuous, high-volume production of SPC core boards with tight density control (2000–2100 kg/m³), eliminating structural voids and air pockets.
3. Advanced Film Printing & EIR Texture Matching: Chinese print houses utilize 6-color gravure printing presses to produce wood grain film up to 2.0 meters wide with razor-sharp 300 DPI resolution. When paired with synchronised steel pressing plates, the tactile texture directly aligns with visual grain lines (Embossed-in-Register), replicating White Oak, Smoked Walnut, and Reclaimed Teak with 99.4% optical realism.
Scale & Lead-Time Control
Operating 8 continuous extrusion lines yields an annual output exceeding 12 million square meters. Standard custom OEM orders are fulfilled within 7 to 15 days, minimizing pipeline latency for overseas distributors.
Global Compliance Testing
Every export batch undergoes rigorous in-house laboratory testing verified by third-party international agencies (SGS, TÜV Rheinland, Intertek) to meet FloorScore, Greenguard Gold, CE, and ISO14001 standards.
Custom OEM & Private Label
Complete flexibility in plank dimensioning (7"x48", 9"x60", 12"x24", Herringbone), customized wear layer thickness (12mil to 28mil), private label carton branding, and pre-attached acoustic underlayments.
3. Micro-Engineering: Anatomical Structure of Wood-Look Vinyl
To understand why vinyl tile that looks like wood outperforms traditional timber, one must evaluate its multi-layer cross-sectional architecture engineered for heavy mechanical load and environmental wear.
Layer 1: Double UV Polyurethane
Infused with microscopic ceramic bead additives. Provides stain resistance, UV color fastness (Grade 6+ ISO 105-B02), anti-bacterial protection, and matte optical tuning (5-7% gloss level).
Layer 2: Clear Wear Layer
High-density transparent virgin PVC film ranging from 0.3mm (12mil) for residential to 0.7mm (28mil) for heavy commercial foot traffic. Standardizes scratch resistance under ASTM F1700 Class III.
Layer 3: 3D High-Def Decor Film
Polymeric printed film captured from natural hardwood timber planks. Utilizes high-stability organic pigments resistant to photo-bleaching and thermal discoloration.
Layer 4: Rigid SPC Core Matrix
High-density limestone composite matrix providing extreme structural rigidity, impact resistance, and water immunity. Eliminates subfloor telegraphing.
Layer 5: Acoustic Underlayment
Pre-attached 1.0mm–2.0mm High-Density IXPE or EVA foam underlay pad. Increases walking comfort, masks minor subfloor imperfections, and achieves high sound ratings.
Material Performance matrix: LVT vs. SPC vs. Hardwood vs. Laminate
A rigorous comparative analysis to assist specification teams in selecting optimal flooring substrates for targeted commercial and residential deployment.
| Performance Parameter | SPC Rigid Core (Wood-Look) | LVT Flexible Tile (Glue-Down) | Natural Engineered Hardwood | High-Density Laminate |
|---|---|---|---|---|
| Water Immunity | 100% Waterproof (Zero Swell) | 100% Waterproof (Surface) | Poor (Swells & Warps) | Moderate (Edge Swelling Risk) |
| Core Density | 2,000 – 2,100 kg/m³ | 1,350 – 1,450 kg/m³ | 650 – 800 kg/m³ | 850 – 950 kg/m³ |
| Subfloor Telegraphing | None (Rigid Core Spans Defects) | High (Requires Ultra-Smooth Concrete) | Moderate | Low |
| Indent Resistance (ASTM F1914) | Superior (< 0.05mm residual) | Moderate (Prone to Heavy Furniture) | Low (Dents easily under pressure) | Good |
| Acoustic Rating (IIC / STC) | IIC 72–75 dB (With 1.5mm IXPE) | IIC 62–65 dB (Glued directly) | IIC 50–55 dB | IIC 58–62 dB |
| Installation Method | Floating Click-Lock (Unilin 5G) | Full Spread Adhesive / Self-Adhesive | Nail Down / Glue Down | Floating Click-Lock |
| Underfloor Heating Compatibility | Excellent (Up to 27°C / 80°F) | Good (Requires Heat-Resistant Glue) | Restricted (Thermal Drying Risk) | Moderate |
4. Macro Industry Trends & Environmental Sustainability Shifts
The global interior building materials market is currently undergoing a transformative shift driven by stringent environmental regulations, indoor air quality (IAQ) mandates, and circular lifecycle requirements. Major enterprise procurement teams are updating specification metrics to address several critical trends:
A. Elimination of Ortho-Phthalate Plasticizers
Historically, flexible vinyl tile relied on phthalate plasticizers (e.g., DEHP, DBP) to achieve core flexibility. Modern Chinese Tier-1 manufacturing facilities have fully transitioned to DOTP (Dioctyl Terephthalate) non-phthalate plasticizers and bio-based soya oil derivatives. This transition ensures compliance with European REACH regulations, US Consumer Product Safety Improvement Act (CPSIA), and California Proposition 65.
B. Ultra-Low VOC Emissions & Indoor Air Quality (IAQ)
Commercial real estate projects seeking LEED v4.1 certification demand flooring materials with near-zero volatile organic compound emissions. Our wood-look vinyl products feature advanced thermal pressing and low-emission UV coatings, achieving FloorScore® and Greenguard Gold certifications. Total Volatile Organic Compound (TVOC) emissions measure less than 0.22 mg/m³ after 28 days of chamber testing under CDPH Standard Method v1.2.
C. Closed-Loop Circular Recycling
Sustainability mandates require manufacturers to incorporate post-industrial vinyl scrap back into structural base layer extrusions without compromising dimensional tensile strength. By utilizing clean, internally recycled edge trimmings, factory production lines reduce virgin PVC polymer usage while guaranteeing 100% heavy-metal-free (Lead, Cadmium, Hexavalent Chromium) structural core integrity.
Hyper-Realistic EIR Optical Tech
Advancements in synchronized laser engraving permit deep tactile pore matching, ultra-matte micro-bevel edges, and low-repeat grain patterns (up to 12 unique plank prints per decors).
Anti-Microbial Nanotech Coatings
Integration of non-leaching silver ion (Ag+) antimicrobial technology directly into the UV topcoat prevents 99.9% of bacterial growth (E. coli, MRSA) per ISO 22196 standards.
Extra-Large Format Planks
Growing market demand for architectural scale planks—reaching 9" x 60" (228mm x 1524mm) and 9" x 72" (228mm x 1828mm)—creating expansive luxury visuals in hotel lobbies and office plazas.
5. Localized Architectural Application Scenarios & Tailored Solutions
Wood-look vinyl flooring provides specialized performance solutions tailored to the operational demands of distinct commercial and residential sectors:
Multi-Family & BTR Developments
Challenge: High tenant turnover, footstep impact noise transmission, subfloor unevenness across large floorplates.
Solution: 4.0mm – 5.0mm SPC click flooring with 1.5mm IXPE acoustic underlayment. Provides fast turnarounds without wet adhesives, achieves IIC 73 sound isolation, and resists heavy rolling loads from moving furniture.
Hospitality & Hotel Interior Design
Challenge: Need for high-end wood aesthetics in guest rooms and corridors coupled with 24/7 moisture exposures and luggage rolling wear.
Solution: 0.5mm (20mil) wear layer dry-back LVT or high-density SPC featuring deep EIR European Oak decors. Delivers warm tactile acoustics, zero moisture damage from spilled beverages or housekeeping cleaning, and easy individual plank replacement.
Healthcare & Assisted Living Facilities
Challenge: Heavy hospital bed wheel loads, strict hygienic sanitation protocols, slip prevention for senior residents.
Solution: Direct glue-down LVT with heat-welded seamless installations or tight click SPC with anti-microbial surface treatments. Certified slip resistance (R10 / DIN 51130) prevents accidental slips while allowing smooth rolling resistance for wheelchairs.
Retail Chains & Shopping Malls
Challenge: Extreme foot traffic abrasion, high point loading from display racks, aggressive daily cleaning routines.
Solution: Heavy-duty 0.7mm (28mil) wear layer SPC featuring double-cured polyurethane coatings with aluminum oxide additive. Prevents scratch whitening and preserves wood visual clarity under 1,000+ Lux retail lighting.
6. Global Corporate Procurement & Supply Chain Risk Management
Sourcing wholesale vinyl tile that looks like wood directly from China requires structured procurement protocols to optimize container utilization, mitigate ocean freight logistics risks, and verify quality control before port dispatch.
A. Container Load Optimization & Packaging Specs
Vinyl flooring products possess high mass-to-volume density. Standard 20-foot Heavy Duty (FCL) shipping containers are utilized to maximize weight capacities (typically capped at 21,000 kg to 27,000 kg depending on regional port road weight limits):
- 4.0mm SPC Plank (No Underlay): ~2,500 – 2,800 m² per 20ft container (approx. 18–20 heavy wooden pallets).
- 5.0mm SPC Plank (with 1.0mm IXPE Pad): ~2,000 – 2,200 m² per 20ft container.
- 2.0mm Dry-Back LVT Plank: ~3,800 – 4,200 m² per 20ft container.
B. Quality Assurance (QA) & On-Site Testing Metrics
Enterprise buyers should require factory pre-shipment inspection (PSI) reports covering key standardized testing parameters:
Click Joint Tensile Strength
Tested per ISO 24334. The long-side and short-side click locking profiles must resist horizontal separation forces exceeding 1.5 kN/m to guarantee seamless floating performance under expansion stress.
Castor Chair Resistance
Tested under EN 425 (25,000 cycles with hard castor wheels). Evaluates surface delamination, wear layer abrasion, or core cracking under dynamic repetitive point loads.
Thermal Stability & Curling
Tested per ASTM F2199 after exposure to 80°C (176°F) for 6 hours. Maximum dimensional movement must remain under 0.15%, with vertical corner curling controlled under 0.5mm.
Wholesale Wood-Look Vinyl & Construction Panels
Select a product line below to inspect engineering specifications, request physical sample binders, or obtain factory-direct ocean container pricing.
Frequently Asked Questions (FAQ) for Enterprise Buyers
Expert engineering answers regarding material selection, factory customization, shipping logistics, and job site installation standards.
LVT (Luxury Vinyl Tile) is a flexible vinyl surface composed of multiple PVC layers plasticized for flexibility, typically installed via full-spread adhesive or loose-lay methods. SPC (Stone Plastic Composite) features a rigid core combining natural limestone powder (Calcium Carbonate) with virgin PVC polymer. SPC delivers significantly higher core density (~2050 kg/m³ vs ~1400 kg/m³ for LVT), superior dimensional stability under thermal variations, 100% waterproof performance, and floating click-lock installation directly over minor subfloor imperfections without telegraphing.
EIR is an advanced manufacturing alignment process where the physical texture embossed into the clear wear layer perfectly matches the visual print of the underlying 3D decorative wood grain film. Using optical sensor-guided steel pressing plates during thermal lamination, cathedral patterns, wood knots, and grain lines receive exact tactile depth, creating an authentic timber finish indistinguishable from natural oak or walnut under direct light.
For standard residential projects, a 0.3mm (12 mil) wear layer is sufficient. Multi-family living, boutique retail, and light commercial spaces require a 0.5mm (20 mil) wear layer. High-traffic commercial environments—such as airport concourses, hospital corridors, university halls, and mega retail centers—demand a 0.7mm (28 mil) wear layer enhanced with micro-ceramic oxide UV coatings to meet ASTM F1700 Class III heavy commercial requirements.
Yes. SPC rigid core flooring exhibits excellent thermal conductivity and dimensional stability due to its dense limestone base. It is certified for installation over hydronic or electric embedded radiant heating systems, provided the surface temperature does not exceed 27°C (80°F). The strict thermal expansion coefficient (< 0.08%) prevents joint opening or plank buckling during seasonal heating cycles.
Bare SPC or LVT installed over concrete slabs yields modest acoustic damping (IIC ~45-50 dB). However, when factory-laminated with a 1.5mm High-Density IXPE closed-cell acoustic underlayment pad, impact sound transmission improves drastically. Standard testing over a 6-inch concrete slab with suspended drywall ceiling achieves Impact Insulation Class (IIC) ratings of 72 to 75 dB and Sound Transmission Class (STC) ratings of 70 to 73 dB, exceeding multi-family building code requirements (IBC Section 1206).
Our typical factory production lead time is 7 to 15 days following container deposit confirmation. Minimum order quantities for standard stocking wood decors start at 500 square meters per color, while fully customized OEM orders (custom plank sizing, specialized wear layer, private label packaging) carry a 1x20' FCL container MOQ (~2,500 m²). We offer turnkey design, custom color lab matching, and custom carton artwork for global brand distributors.
All production batches utilize 100% virgin PVC polymer and refined natural limestone powder completely free of lead, cadmium, mercury, and phthalates. Products undergo rigorous laboratory screening for chemical compliance under EU REACH, California Proposition 65, and French VOC Regulation (A+ Class), holding active FloorScore® and Greenguard Gold certifications for healthy indoor air quality.
Every extrusion batch undergoes strict 24-hour quality control protocols: 1) Dimensional tolerance and squareness checks (±0.15mm), 2) Wear layer micro-scratch testing, 3) High-temperature thermal oven testing (80°C for 6 hours) to measure expansion and curling, 4) Unilin click joint pull-strength tensile testing (ISO 24334), and 5) Gloss level consistency checks across all running rolls.